What project owners need to know.
Ingot-to-wafer yield is the share of the silicon charged into a crystal puller that ends up as good, sellable wafers. Silicon leaves the chain at five main points: melt left in the crucible at the end of a Czochralski pull, the crown and tail cropped off the ingot, the side slabs removed when a round ingot is squared into bricks, kerf turned to powder by the wire saw, and wafers rejected or broken at inspection. The losses are not equal. Crop ends, squaring off-cuts and clean melt residue are solid silicon that is commonly cleaned and remelted, so they lower throughput more than they waste material. Kerf is different: a 2024 review of diamond-wire saw silicon powder reports that roughly 35 to 45% of the silicon entering the sawing step leaves as fine particles in the cutting fluid, and almost none of it returns to the ingot today. There is no single industry-wide yield figure; it depends on ingot diameter and length, wafer format and thickness, wire diameter, crystal quality and plant discipline.
Why yield matters as much as silicon price
Polysilicon is bought by the kilogram but wafers are sold by the piece. Every kilogram that does not become a good wafer still had to be bought, melted and, in many cases, grown and cut. That is why ingot and wafer plants watch yield at each station rather than only the price of their feedstock.
It also explains why the same pulling and slicing equipment can perform very differently in two plants. Hot-zone control, cropping discipline, saw set-up and handling all move the share of the charge that becomes sellable wafers. This guide maps the stages qualitatively; it deliberately does not give a universal percentage, because published figures depend on assumptions that rarely match a specific line.
Stage 1: the charge and what stays in the crucible
In batch Czochralski growth, polysilicon and dopant are melted in a fused-quartz crucible and a single crystal is pulled from the melt. The pull is normally stopped before the crucible is empty, so some silicon remains as melt residue that freezes in the crucible. Impurities that the growing crystal rejects concentrate in that last melt, which is one reason it is not pulled to the very end.
Recharge Czochralski (RCz) and continuous Czochralski (CCz) change this picture by adding fresh polysilicon to the hot crucible so that several ingots are grown before the crucible is retired, spreading the residue and the crucible itself over more output.
- Melt residue: solid silicon, but it carries the most concentrated impurities
- The crucible is a single-use consumable in batch Cz
- Multiple pulls per crucible (RCz/CCz) reduce residue per ingot
Stage 2: crown, tail and off-specification sections
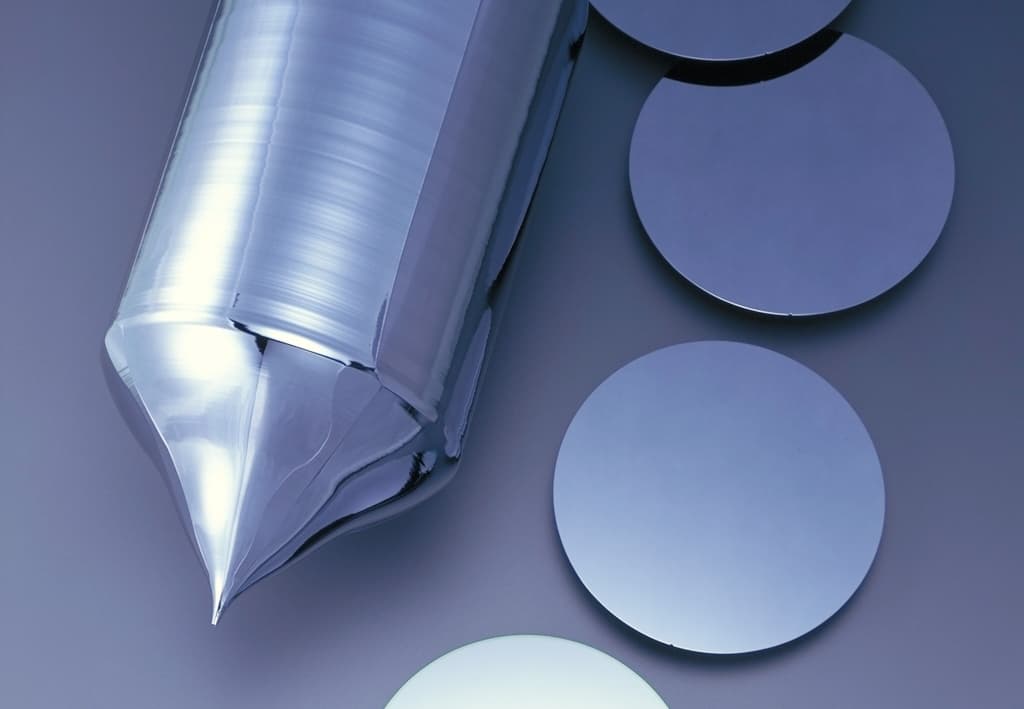
A Czochralski ingot starts with a thin neck and a shoulder that widens to full diameter, and it finishes with a tapered tail cone. Neither end has the full diameter needed for wafers, so both are cropped. Any length of the body that falls outside the resistivity, lifetime or dislocation specification can also be cut out at this stage.
These crop ends are solid, relatively clean silicon. In practice they are commonly cleaned, etched and returned to later melts, so they reduce how many wafers each pull yields without being lost to the plant.
Stage 3: squaring the round ingot into bricks
Solar cells are tiled edge to edge in a module, so the round ingot is cut into a near-square brick before slicing. Four side slabs are removed, leaving the small chamfered corners that show where the round ingot used to be. Chip wafers skip this step and are ground to an exact round diameter instead.
The size of the side slabs depends on how closely the ingot diameter is matched to the target wafer format. Like crop ends, squaring off-cuts are solid silicon that can usually be recycled into the melt.
Stage 4: wire-saw kerf, the loss that does not come back
Each cut of the diamond wire turns a slice of silicon roughly the width of the wire and its abrasive into fine powder. Because the wire pitch is the wafer thickness plus the kerf, kerf is lost on every single wafer in the brick, which is why it is the largest material loss in the chain.
A 2024 review of silicon recovery from diamond-wire saw powder reports that about 35 to 45% of the silicon entering sawing leaves as waste particles in the cutting fluid, with an average particle size around 0.5 µm. The powder is fine, oxidised at the surface and mixed with coolant and diamond-wire debris, so it is not simply remelted. Recovery research is active, but today this silicon is largely lost to the ingot route. Thinner wires reduce kerf, and kerfless approaches avoid it entirely.
Stage 5: breakage, rejects and grading
After slicing, wafers are de-glued, cleaned, dried and inspected for thickness, thickness variation, saw marks, chips, cracks and electrical properties. Wafers that break in handling or fall outside specification reduce yield at the very end of the chain, after all the earlier cost has been spent.
Thinner wafers save silicon per wafer but are more fragile, so breakage control in handling, cleaning and automation becomes part of the yield equation rather than a separate issue.
What can be recovered and what cannot
The useful way to read the chain is to separate solid losses from powder losses. Solid silicon, such as crop ends, squaring off-cuts and clean melt residue, is normally cleaned and recycled into the furnace, subject to purity control. Powder losses, chiefly kerf, are not recovered into the ingot route today.
- Usually remelted: crop ends, squaring side slabs, clean melt residue, broken ingot pieces
- Usually lost: wire-saw kerf powder
- Depends on purity: melt residue from the end of a pull, rejected wafers
- Levers: diameter-to-format matching, multiple pulls per crucible, thinner wire, careful handling
How JRST supports this requirement
JRST works across the quartz-to-wafer chain, from high-purity quartz sand and crucibles to Czochralski ingot growth and wafering, and can help a plant map where its silicon is going station by station. Buyers looking for pullers, wafering equipment, crucibles or spare parts can browse the JRST Buyer Portal from the matching product pages. Any yield target is plant-specific and should be validated against the actual line, feedstock and wafer specification.
Discuss your requirement
Mohammed Saif Zaveri connects JRST's industrial content to execution conversations.
As Co-Founder and designated partner of JRST Technology LLP, Mohammed Saif Zaveri works across industrial growth, strategic partnerships, client conversations, equipment strategy, and project pathways for silicon, solar, semiconductor, and advanced-manufacturing opportunities.
This knowledge page is part of JRST's public industrial knowledge base, designed to help buyers move from search terms and early research toward a structured technical-commercial discussion.
View Mohammed Saif Zaveri's profileConnect on LinkedInFrequently asked questions
What is ingot-to-wafer yield?
It is the share of the silicon charged into a crystal puller that ends up as good, sellable wafers. It is reduced by melt residue, crop ends, squaring off-cuts, wire-saw kerf and wafer rejects.
Where is most silicon lost in wafer manufacturing?
Wire-saw kerf is the largest loss that is not recovered. A 2024 review reports roughly 35 to 45% of the silicon entering diamond-wire sawing leaves as fine powder in the cutting fluid. Crop ends and squaring off-cuts are also large, but they are solid silicon that is usually remelted.
Is kerf loss recoverable?
Not into the ingot route today. Kerf powder is very fine, surface-oxidised and mixed with coolant and wire debris. Research into recovering it is active, but most plants treat it as waste.
Why are solar ingots squared before slicing?
Solar cells are tiled edge to edge in a module, so a near-square wafer uses module area better than a round one. Squaring removes four side slabs from the round ingot, which are usually recycled into later melts.
What share of the polysilicon charge becomes wafers?
There is no single public figure that applies to every plant. It depends on ingot diameter and length, wafer format and thickness, wire diameter, crystal quality, how many ingots are grown per crucible and handling discipline, so any quoted number should be read with its assumptions.
Primary sources and further reading
Last reviewed 2026-11-20. Technical scope, policy eligibility, availability, and commercial terms should be independently confirmed for each project.