What project owners need to know.
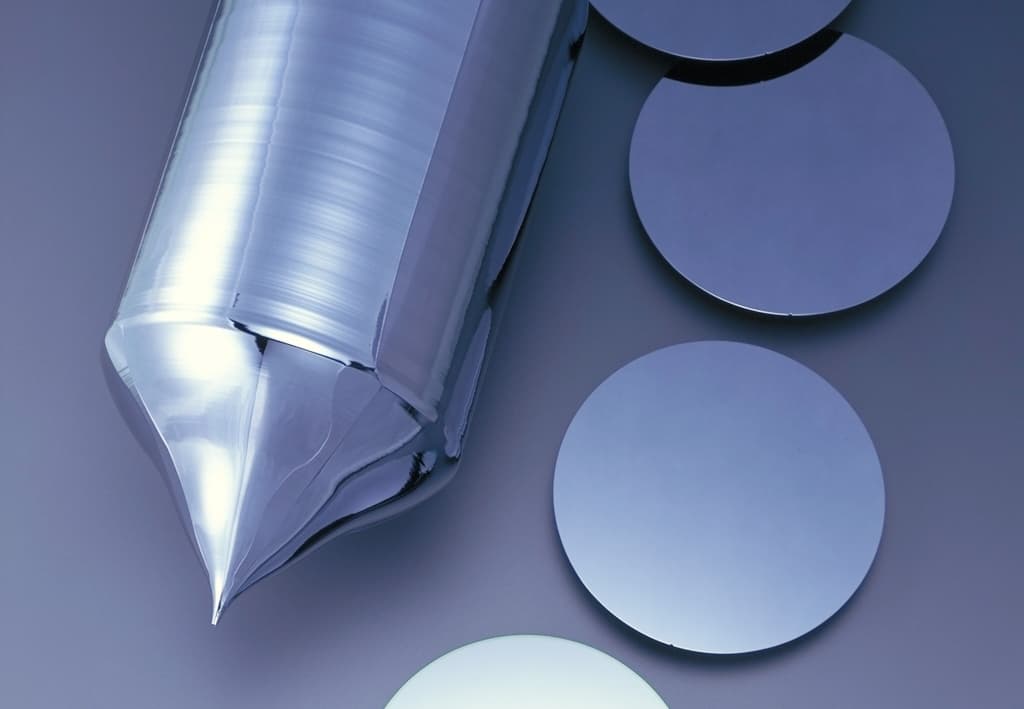
Wafer slicing is usually pictured as one machine cutting an ingot. In production it is a sequence of stations, and the slicer is only one of them. A grown ingot is cropped and squared into bricks, ground to dimension, bonded to a mounting beam, cut by diamond wire into hundreds of wafers still attached to that beam, then pre-cleaned, deglued off the beam, separated into individual wafers, dried and inspected. Each station sets something the later ones cannot recover. Brick geometry fixes the achievable thickness uniformity; the bond decides whether wafers move during the cut; the cut sets the subsurface damage; and the separation sequence decides how many thin wafers survive handling. Understanding the chain, rather than the saw, is what makes a wafering line specifiable.
The slicer is one station in a sequence
A wafering line takes a cylindrical grown ingot and returns clean, separated, inspected wafers. Between those two points sit cropping, squaring, grinding, bonding, the cut, pre-cleaning, degluing, singulation, drying and inspection. Buyers who evaluate a wafering line by comparing slicers are comparing one station and assuming the rest.
The cut itself is well understood and covered separately in our diamond-wire guide. In short, PV-Manufacturing.org records that the industry has moved fully from slurry sawing — which used hard steel wire around 180 µm thick and produced roughly 200 µm of kerf — to fixed-abrasive diamond wire, which cuts a narrower kerf, runs faster and leaves roughly half the saw damage. Wire spacing on the web sets the wafer thickness. Trade analysis from August 2022 reported production wire at 36–40 µm, down from 42–47 µm in the first half of 2021, with some lines already on 32 µm tungsten-core wire.
What follows here is everything either side of that cut, because that is where most avoidable yield is lost.
- Evaluate the line as a sequence, not as a slicer plus accessories
- Ask which stations are in the vendor's scope and which are assumed
- Wire spacing sets thickness; wire diameter sets kerf
- Handling steps, not the cut, dominate breakage on thin wafers
Brick preparation decides the wafer before any cut is made
A grown ingot is not ready to slice. Its ends carry the seed and tail cones, where resistivity and crystal quality sit outside specification, so they are cropped off. The round body is then squared into a pseudo-square brick matching the target wafer format, and ground to final dimension so that every brick entering the saw presents the same geometry.
This stage is quietly decisive. If bricks vary in dimension or squareness, the wire web meets a different workpiece each run, and thickness uniformity and total thickness variation drift even with identical saw settings. Cropping also determines how much of the ingot becomes saleable wafer at all, because the cropped material returns to feedstock rather than to a customer. Where the crop lines are drawn is a resistivity and lifetime decision, which is why measurement at brick stage — rather than argument at wafer stage — is worth building in.
- Crop on measured resistivity and lifetime, not on a fixed length
- Hold brick dimension and squareness tolerances tightly and monitor drift
- Treat cropped and squared material as a recovery stream, not scrap
- Measure at brick stage so wafer-stage rejects can be traced back
Mounting: the step nobody specifies and everyone blames
Before cutting, the brick is bonded to a mounting beam — a sacrificial carrier that holds the workpiece through the cut and, critically, holds every resulting wafer in place afterwards. Without it, the moment the wire passes through, hundreds of thin wafers would separate under their own weight.
The bond has to survive the mechanical load and the coolant flow of the entire cut, then release cleanly and completely on demand. Those are opposing requirements, and they are why the adhesive and beam are a genuine specification rather than a shop-floor consumable choice. A bond that is too weak allows movement during the cut, which shows up as thickness variation and saw marks. A bond that releases poorly extends the degluing step, leaves residue that the cleaning chemistry must then remove, and raises handling breakage on wafers already thinned toward 130 µm.
- Specify the adhesive and beam, do not inherit them from the saw vendor
- Test bond release and residue, not only bond strength
- Correlate thickness variation against mounting batches before blaming the saw
- Confirm beam reuse limits and how reuse is tracked
After the cut: pre-clean, deglue, singulate, dry
When the wire finishes, the output is not wafers but a cut block: hundreds of slices still held on the beam and coated in cutting fluid and silicon fines. A published wafer-manufacturing patent describes the sequence that follows in useful detail. The block is first pre-cleaned while still mounted, with water alone or with added surfactant or organic substance, at 10–45 °C and typically 20–35 °C, to remove the sawing residue before anything is separated.
Only then does degluing take place, in a basin at 60–100 °C and typically 70–95 °C, using water with or without surfactant or a mixture of water with an organic acid, which dissolves the adhesive and releases the slices from the saw holder. The same patent notes that slices heated to 70–90 °C are kept from drying on the surface by spraying with warmed solution, then moved to a cooling basin at 40–60 °C.
The sequencing point is the one worth carrying away: that patent's stated innovation is that singulation — separating the stack into individual wafers — happens only after pre-cleaning, precisely to avoid damaging thin wafers while they are still dirty and fragile. Order of operations, not equipment specification, is what protects yield here.
- Pre-clean before separating, not after
- Control degluing temperature and residence time as process parameters
- Prevent surface drying between stations — dried residue becomes a defect
- Design wet handling for the thickness you will run in three years, not today
The damage you ship is the damage your customer removes
Every cut leaves a damaged layer beneath the wafer surface. A 2024 study in Materials measured subsurface microcrack damage depths of roughly 9.7 to 15.9 µm across its test conditions and proposed predicting that depth from as-sawn surface roughness, reporting the relationship SSD = 21.179 × Ra^(4/3) with accuracy within about 5% relative error. Its parameters were laboratory ones — a 120 µm core wire with 15–20 µm abrasive on 0.5 mm wafers — so the numbers should not be read as production values, but the principle holds: roughness is a usable proxy for damage you cannot see.
The commercial consequence is that this damage is removed on the cell line, not the wafer line. PV-Manufacturing.org is explicit that sawing damage must be removed during solar cell manufacturing and that failing to do so reduces minority carrier lifetime and therefore cell efficiency, with alkaline etching the common route — suggested settings of 20–40% w/v sodium hydroxide at 30–70 °C for 5–15 minutes, an anisotropic etch whose rate falls as silicate builds up in the bath.
So the wafer maker creates the damage and the cell maker pays to remove it, in silicon thickness, chemistry and time. That makes as-sawn surface quality a commercial term, not just a process outcome. Indian wafer projects selling into domestic cell lines ahead of ALMM List-III should expect roughness and damage to be negotiated, and should be measuring both long before a customer asks.
- Measure as-sawn roughness routinely and keep it per lot
- Expect cell customers to negotiate damage depth, not just thickness
- Do not read laboratory SSD figures as your line's values — measure your own
- Link roughness data back to wire age, feed rate and coolant condition
How JRST supports this requirement
JRST supports wafering projects across the whole sequence, not just the saw: brick preparation and measurement strategy, mounting and adhesive specification, wet-process order of operations, and the as-sawn quality terms that sit between a wafer supplier and its cell customers. Figures on this page are drawn from public technical sources, published patents and peer-reviewed literature and should be validated for the specific project; process outcomes depend on material, equipment and settings and must be established by trial.
Discuss your requirement
Mohammed Saif Zaveri connects JRST's industrial content to execution conversations.
As Co-Founder and designated partner of JRST Technology LLP, Mohammed Saif Zaveri works across industrial growth, strategic partnerships, client conversations, equipment strategy, and project pathways for silicon, solar, semiconductor, and advanced-manufacturing opportunities.
This knowledge page is part of JRST's public industrial knowledge base, designed to help buyers move from search terms and early research toward a structured technical-commercial discussion.
View Mohammed Saif Zaveri's profileConnect on LinkedInFrequently asked questions
What are the steps in the wafer slicing process?
Cropping and squaring the ingot into bricks, grinding to dimension, bonding the brick to a mounting beam, cutting with diamond wire, pre-cleaning the cut block, degluing it off the beam, separating the wafers, drying and inspecting them.
Why is the ingot cropped and squared before slicing?
The seed and tail ends fall outside resistivity and crystal-quality specification and are removed. Squaring and grinding produce a pseudo-square brick of consistent dimension so that every brick presents the same geometry to the wire web.
What holds the wafers together during slicing?
The brick is bonded to a sacrificial mounting beam. It carries the workpiece through the cut and holds each wafer in place afterwards; without it the slices would separate under their own weight as soon as the wire passed through.
What is degluing in wafer manufacturing?
Dissolving the adhesive that bonds the cut block to its mounting beam so the wafers release. A published patent describes a basin at 60–100 °C, typically 70–95 °C, using water with surfactant or water mixed with an organic acid.
When are wafers separated from each other?
After pre-cleaning, not before. Separating a stack that still carries cutting residue risks damaging thin wafers, so pre-cleaning while the block is still mounted, then degluing, then singulating, is the sequence that protects yield.
Is saw damage removed on the wafer line or the cell line?
On the cell line. PV-Manufacturing.org describes saw damage removal as part of solar cell manufacturing, commonly by alkaline etching, and notes that skipping it reduces minority carrier lifetime and cell efficiency.
How can JRST help with a wafering line?
JRST can help scope the full station sequence rather than the saw alone, set brick, mounting and wet-process specifications, and frame as-sawn quality terms with cell customers. Line performance is project-specific and must be established by trial and measurement.
Primary sources and further reading
Last reviewed 2026-09-22. Technical scope, policy eligibility, availability, and commercial terms should be independently confirmed for each project.